01
Gentle ampoule wrap-around labeling
The Ampoule Sticker Labeling Machine is intended for approved fragile cylindrical glass ampoules; performance is assessed against the output and acceptance criteria stated for the approved configuration.
Apply full or partial wrap-around self-adhesive labels to approved fragile cylindrical glass ampoules. Selection focuses on ampoule diameter, label size, gentle feeding, controlled spacing and rotation, and transfer to tray collection or downstream packing.
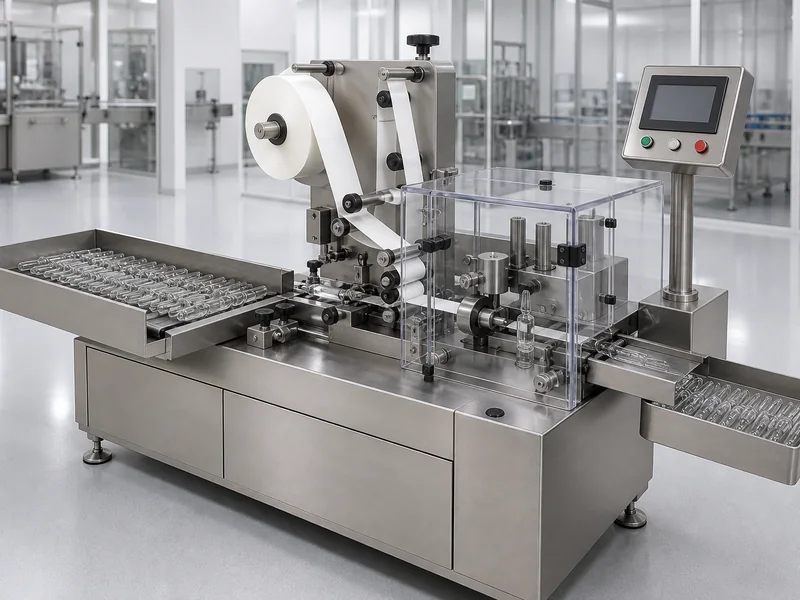
Machine overview
H M Pharma Machines manufactures the Ampoule Sticker Labeling Machine in Ahmedabad, Gujarat, India for approved fragile cylindrical glass ampoules.
Ampoules are separated through the selected worm, star wheel or horizontal roller arrangement, sensed and rotated to complete the approved label wrap. Tray, conveyor or worm feeding is matched to the required ampoule pitch.
The approved ampoule and label samples determine the handling architecture, output and placement acceptance basis. Coding, camera inspection and rejection are configurable; collection must also be reviewed with the downstream packing requirement.
Why this machine
The Ampoule Sticker Labeling Machine is intended for approved fragile cylindrical glass ampoules; performance is assessed against the output and acceptance criteria stated for the approved configuration.
Gentle tray, conveyor or worm feeding with positive ampoule pitch.
Label-web, product-sensor, handling-speed and recipe controls.
For the Ampoule Sticker Labeling Machine, the materials and cleanability review follows this product-contact requirement: Container guides, label-contact rollers, guards and conveyor materials are selected from approved product and label samples.
Ampoule-format changeover covers the feed pitch, handling guides, label-web path, dispenser setting and sensor position for the approved ampoule and label.
Labeled ampoules discharge to tray collection or downstream packing.
Operating process
Fragile cylindrical ampoules are gently pitched, sensed and rotated under control while a self-adhesive label is dispensed and wrapped around the glass body.
Ampoules enter from the tray, conveyor or worm-feed arrangement and are guided without uncontrolled glass-to-glass pressure.
The configured worm, star wheel or roller system establishes ampoule pitch, and the product sensor triggers one label for the registered body.
The label peels from its backing onto the ampoule, which rotates between supported contact surfaces to complete a smooth circumferential wrap.
The applied ampoule is released gently to tray collection, inspection or the configured downstream packing equipment.
Applications & selection
Provide actual ampoules with diameter, height and the required label position so the handling parts and label application can be reviewed together.
Confirm label dimensions, stock and wrap position on the cylindrical body. The approved label and ampoule samples define suitability.
State whether ampoules arrive by tray, conveyor or the proposed worm feed. Positive pitch and gentle transfer are part of the configuration review.
Confirm the selected handling architecture from the ampoule sample, infeed arrangement and collection requirement; the approved drawing defines the supplied layout.
Specify whether coding, camera inspection and reject handling are required so they are included in the approved scope.
Confirm how labeled ampoules are collected and transferred to the next packing step. The labeler can operate independently or connect to the approved line.
Output, ampoule and label dimensions, roll/core ranges, placement tolerance and FAT method remain configuration-specific. Confirm these against the actual samples in the machine datasheet and quotation; no universal size or speed rating is implied.
Technical details
| Machine | Ampoule Sticker Labeling Machine |
|---|---|
| Category | Labeling Machines |
| Suitable For | Approved fragile cylindrical glass ampoules |
| Working Principle | Ampoules are separated by a worm, star wheel or horizontal roller system, a label is dispensed and controlled rotation completes the wrap. |
| Infeed / Handling | Gentle tray, conveyor or worm feeding with positive ampoule pitch |
| Outfeed / Transfer | Labeled ampoules discharge to tray collection or downstream packing |
| Machine Construction | GMP-oriented stainless-steel construction as defined in the approved scope |
|---|---|
| Contact Materials | Container guides, label-contact rollers, guards and conveyor materials are selected from approved product and label samples. |
| Control System | Label-web, product-sensor, handling-speed and recipe controls |
| Changeover | Settings, guides and format parts matched to approved samples or drawings |
| Optional Scope | Vertical or horizontal architecture, coding, camera inspection and reject are configurable. |
| Line Integration | Standalone supply or integration with approved upstream and downstream machines |
| Machine configuration | Ampoule wrap-around labeler; vertical or horizontal handling and the assigned model code are identified in the quotation. |
|---|---|
| Ampoule and label formats | Approve glass-body diameter, height, label position, label dimensions, stock, roll diameter and core from actual samples. |
| Feeding and collection | Select tray, conveyor or worm feeding with controlled ampoule pitch; define tray collection or the downstream packing interface. |
| Output assessment | Agree ampoules per minute for the selected feed, glass-body format, label web and handling arrangement after sample trials. |
| Label placement and FAT | Define placement tolerance, wrap position and the sampling method using the approved ampoules and labels at the agreed running rate. |
| Published control reference | Delta PLC, 4-inch Delta HMI and Delta drive/VFD; Delta servo applies where servo motion is included in the ordered arrangement. |
| Electrical and pneumatic services | The load list states supply voltage, phase, frequency and connected load; compressed air is required only for fitted pneumatic actuators. |
| Format changes | Document the guides, worm, star wheel or roller parts and label-head settings required for each approved ampoule format. |
| Footprint and access | The approved GA drawing defines overall dimensions, feed and discharge heights, roll-change access and integration clearances. |
| Net and shipping weight | The final datasheet and packing list state machine and packed weights for the selected handling architecture. |
| Warranty | Published reference: 1 year. Commencement, coverage and exclusions follow the approved order terms. |
| Installation and commissioning | Available under the approved order; define setup, line interfaces, sample trials, training and customer utility responsibilities. |
Final specifications follow the approved quotation, layout, datasheet and project URS.
Options & project scope
Approved fragile cylindrical glass ampoules.
Vertical or horizontal architecture, coding, camera inspection and reject are configurable.
Documentation for the Ampoule Sticker Labeling Machine records label-web, product-sensor, handling-speed and recipe controls, the confirmed utilities and the agreed acceptance tests; drawings, manuals and qualification records are supplied when ordered.
Controls & protection
Controls, alarms and interfaces are confirmed for the ordered configuration.
Label-web, product-sensor, handling-speed and recipe controls.
Infeed readiness: gentle tray, conveyor or worm feeding with positive ampoule pitch.
Approved transfer: labeled ampoules discharge to tray collection or downstream packing.
Configuration-specific: Electrical supply is required; compressed air is listed only for configured actuators, with coding, vision and data interfaces stated separately.
Configuration-specific: Label-placement tolerance and FAT method are confirmed after approved container-and-label sample trials.
Vertical or horizontal architecture, coding, camera inspection and reject are configurable.
Frequently asked questions
The Ampoule Sticker Labeling Machine applies full or partial self-adhesive labels to ampoules using synchronized gentle handling.
Suitable products and formats include approved fragile cylindrical glass ampoules. Final suitability is confirmed from approved samples, drawings and process details.
Ampoules are separated by a worm, star wheel or horizontal roller system, a label is dispensed and controlled rotation completes the wrap.
The Ampoule Sticker Labeling Machine handles material using gentle tray, conveyor or worm feeding with positive ampoule pitch.
Labeling speed is established from ampoule diameter and length, feed pitch, label length, roll specification, sensor response and the time needed for controlled wrap-around application.
The worm, roller or star wheel setting, support guides, label position and sensor are adjusted or changed to match approved ampoule and label samples without excessive glass-to-glass pressure.
Ampoule-contact guides, worms or rollers and supporting surfaces are chosen to control glass safely, while peel-plate, label-contact and guarding materials suit the approved label web.
The available control scope includes label-web, product-sensor, handling-speed and recipe controls. Final alarms and interlocks are documented in the approved control specification.
Vertical or horizontal architecture, coding, camera inspection and reject are configurable.
It is normally positioned after ampoule inspection and before secondary packing, with optional coding or label-vision inspection located around the application station.
Available documents can include the ampoule-and-label format sheet, web-path and roll-winding drawing, electrical and sensor diagrams, changeover instructions, manuals, layout and labeling FAT report.
Please provide the following: ampoule and label samples, fragility, winding direction, output, coding, vision and collection method.
Contact us
Share your application and required capacity for a quotation.
Confirmed standards
Suitable containers are matched to the approved ampoule and label samples. Output, size range, utilities and dimensions remain subject to the approved machine scope.
Automation uses a Delta PLC, 4-inch Delta HMI and Delta drive/VFD.
Delta servo is used where servo motion is included in the selected configuration.
The confirmed warranty period is one year.
Installation and commissioning are available; the exact scope is defined in the approved order.