In This Guide
- Name the exact bottle and closure combination
- Match each acceptance check to the closing action
- Check ROPP formation as a complete closure
- Separate a tightening setting from a measured result
- Build a closure trial record that another reviewer can follow
- Include interruptions and format changes in acceptance
- Keep head-specific results with the decision
- Buyer Questions
- Related practical guides
- Equipment scope and measurement reference
- Plan a closure acceptance trial
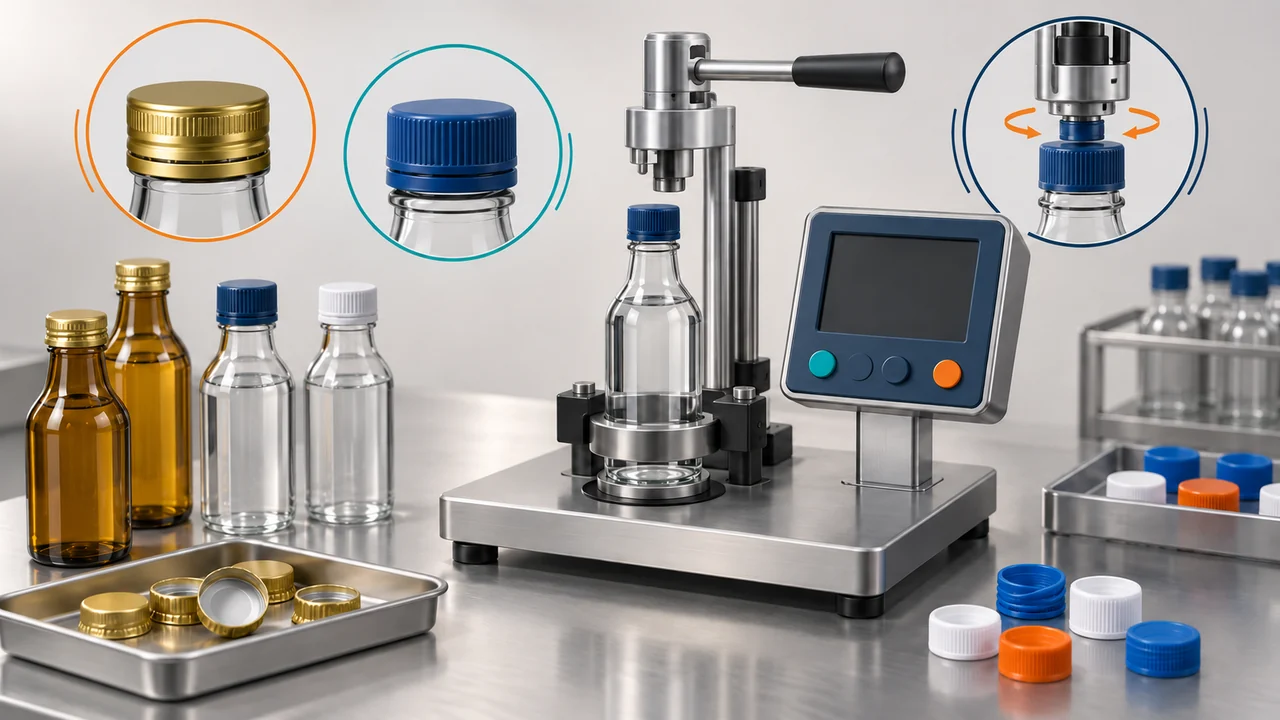
A capping trial needs a finished-closure acceptance plan, not only a machine setting. ROPP forming and screw-cap tightening use different closing actions, while servo torque control is a way to control the selected screw-capping head. This guide explains how to keep those differences clear and prepare practical checks for H M Pharma Machines single-head, multi-head and servo torque configurations.
Agree acceptance with the bottle, cap and process owners before the trial. ROPP needs defined forming and seal checks; screw closures need the specified tightening and finished-closure checks. Record actual component references and the test method. A control setting alone is not proof of closure quality.
Name the exact bottle and closure combination
Supply bottle neck-finish drawings and samples together with the cap, liner and any pilfer-band details. Identify supplier and component revisions. These are part of the trial baseline: changing a closure or neck finish while retaining the same machine settings should trigger a review, not an assumption of equivalent results.
Define the required closed-pack condition with the relevant component and process owners. Separate mechanical appearance, opening behavior and any required seal assessment. No universal torque value or forming setting can be assigned responsibly from a machine name alone.
Match each acceptance check to the closing action
| Closing arrangement | What the machine does | Acceptance focus to define |
|---|---|---|
| Single-head or multi-head ROPP | Top pressure and rollers form the aluminum cap to the neck | Thread and pilfer-band formation, damage and seal criteria |
| Single-head screw capping | A chuck tightens a pre-threaded cap on a supported bottle | Cap seating, opening or torque method and required seal checks |
| Servo torque capping | A servo-controlled head applies the selected screw-capping setting | Finished-closure checks, separately from the control setting |
Single-head and multi-head describe handling and head arrangements. They do not change the need for acceptance criteria for the actual component pair.
Check ROPP formation as a complete closure
The published ROPP platforms apply controlled top pressure while rollers form the cap skirt and pilfer-proof band against the bottle neck finish. Review bottle and neck support, square cap placement and the selected roller setup together. The multi-head platform adds worm, star-wheel and turret handling around that forming action.
Agree how the formed thread, band, cap condition and any seal requirement will be examined. An opening-torque observation alone does not describe every part of a formed ROPP closure. Record which head or station produced a sample when the trial arrangement allows that identification.
Separate a tightening setting from a measured result
A screw-capping head rotates a compatible pre-threaded cap while the bottle is supported against unwanted movement. Review square cap placement, chuck engagement and bottle holding before adjusting the torque or clutch setting. A cap seated incorrectly can give a misleading impression of completion.
The published servo torque machine is an automatic linear single-head platform with HMI torque adjustment. That setting describes the controlled head action; it is not an independent measurement of finished-pack removal torque or seal integrity. Use the defined closure test method to assess the result rather than reading the display as a certificate of acceptance.
Build a closure trial record that another reviewer can follow
Agree the checks, sample plan and acceptance criteria before the run. The buyer identifies the intended pack and process requirement; the bottle and closure suppliers provide the relevant component specifications; the machine supplier records the offered tooling and setup. Name the person who will perform each test and the reviewers who can close the result.
| Record field | What to retain | How the reviewer uses it |
|---|---|---|
| Component baseline | Bottle neck-finish drawing/revision, cap and liner identity, supplier and lot, sample condition | Check that the tested combination matches the requested format. |
| Run and sample identity | Run ID, sample sequence, available head/station ID and startup, steady-run or restart stage | Locate a result without pooling different heads or operating stages. |
| Machine setup | Tooling references and setup revision; HMI or mechanical setting recorded in its stated units | Reproduce the setting without treating it as an independent closure measurement. |
| Assessment method | Specified test, instrument ID and required suitability/calibration evidence; time after capping and relevant conditions | Check that results were obtained by the agreed method under comparable conditions. |
| Separate results | Raw measured value and units where applicable; thread/band/appearance observations; seal-test evidence reference | Compare every required characteristic with its own acceptance criterion. Mark a check not performed rather than leaving a blank. |
| Decision and next action | Accepted scope, unresolved item or retest; action owner, due date and linked repeat-run ID | Close only the requirement supported by the evidence and carry restrictions into the format record. |
For a torque test, specify which event the result represents: for example, the required opening measurement or a defined tamper-band event. The instrument and procedure must support that event. Record the raw result and its units; a note such as “torque OK” loses the evidence needed for comparison. The Mecmesin torque-tester documentation illustrates the distinction between application, removal and bridge/peak measurements. It does not set the acceptance limit for your closure.
Include interruptions and format changes in acceptance
Observe startup and recovery after a planned cap-feed or downstream stop. Review bottle support and cap presentation at restart, including how an unsuitable closure is identified and handled. Cap presence sensing, inspection and automatic rejection should be stated separately in the machine scope.
For each additional format, record the changed guides, support parts, chucks or ROPP forming settings. Retain the acceptance method with that setup record. A successful demonstration on one bottle-cap combination should not be extended to another supplier, closure design or format without the appropriate component and process review.
Keep head-specific results with the decision
Where the supplied arrangement allows safe identification, retain the closing head or station for each sample. Compare the same component lots and assessment conditions. Keep startup, steady-operation and restart samples distinguishable; a repeated issue from one position can disappear in an overall summary. If the head cannot be identified, record “unknown” and ask the supplier for an approved diagnostic method.
- Review the individual evidence: check the required formation, opening and seal results, including any unperformed test. An acceptable appearance or torque result does not close a missing seal assessment.
- Assign the next action: give a repeated head-related observation to the machine supplier for diagnosis; give an unresolved component specification to the responsible bottle or closure supplier. The designated buyer reviewer decides whether the evidence covers the intended pack.
- Record an intervention: retain the original run, the reason for change and the authorized setup revision. Repeat the affected checks under the agreed plan, with new sample IDs. One isolated value is not a basis for an undocumented adjustment.
- Close the tested scope: record the accepted combination and conditions, any restriction, and each outstanding action with its owner. Do not carry the decision to a changed cap, liner, bottle or tooling revision without review.
Buyer Questions
Does a servo torque setting equal removal torque?
No. It is a setting for the controlled capping action. Assess finished-closure removal torque using the specified measurement method and conditions rather than treating the HMI value as an independent result.
Is torque the only acceptance check for ROPP caps?
No. Define thread and pilfer-band formation, component condition and any required seal checks for the actual aluminum cap and neck finish. The plan should reflect the complete closure.
Can a trial result be reused after changing the cap supplier?
Do not assume equivalence. Compare drawings and components, review tooling and settings, and perform the relevant acceptance checks for the revised bottle-cap combination.
Related practical guides
- Plan cap presentation — review cap orientation, pickup and restart before the closing assessment.
- Review the complete change-parts set — identify the supports, chucks or forming parts associated with an accepted format.
- Define inspection and rejection scope — separate closing quality checks from detection and physical segregation.
Equipment scope and measurement reference
The single-head ROPP and multi-head ROPP pages describe the forming arrangements. The single-head screw capper and linear single-head servo torque capper describe screw-closing alternatives. Use the approved offer and component-specific protocol to establish the actual head arrangement, test method and included inspection scope.
Plan a closure acceptance trial
Share the bottle neck-finish drawing, identified cap and liner samples, closing method and the checks you need to witness. Include any open acceptance question so H M Pharma Machines can review the trial scope.
Request a capping trial review