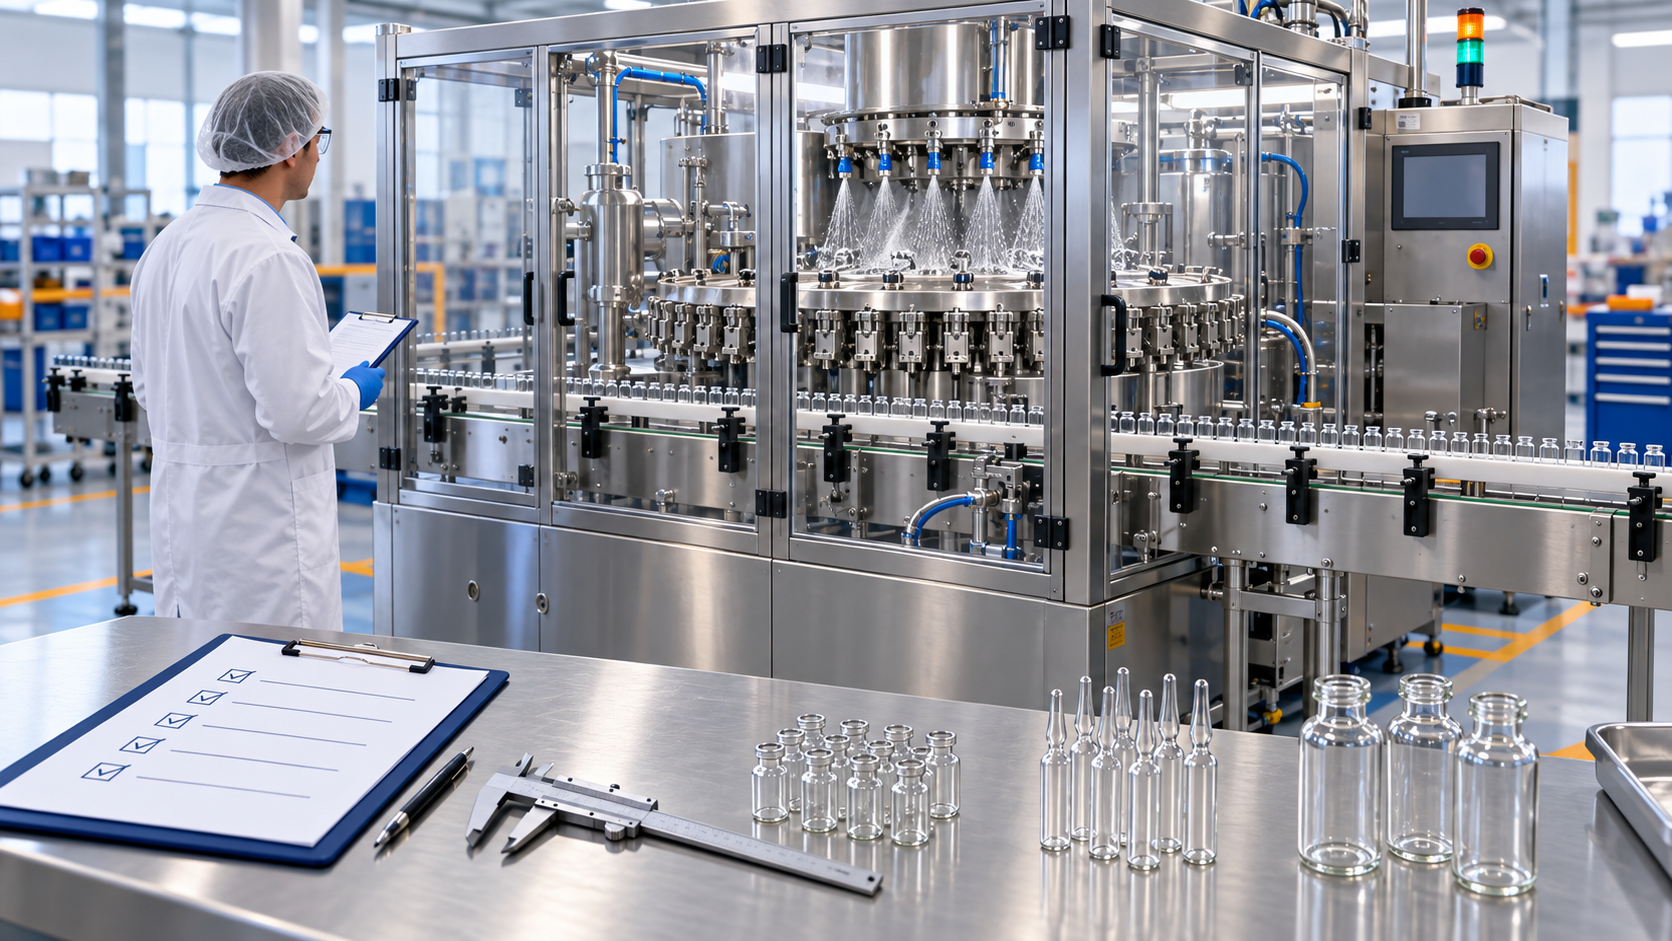
A pharmaceutical washing machine should reach dispatch with an agreed test record, not only a demonstration video or a headline output. This pharmaceutical machinery FAT checklist applies to vial, ampoule and bottle projects. It helps the buyer and supplier agree what will be tested, what evidence will be recorded and how deviations will be closed.
Use the checklist with the selected machine page: the rotary gripper ampoule washing machine is published for 1–20 mL glass ampoules only, while the rotary gripper vial washing machine is published for 2–100 mL glass vials only. The linear tunnel vial washing machine and rotary gripper bottle washing machine have different handling arrangements. The approved order, drawings, samples and URS decide what applies to a particular FAT.
Adapt the Trial to the Container and Machine
Vial washing machine FAT
For a vial washing machine, review the approved vial geometry, rotary-gripper or linear-pocket handling, wash sequence and transfer to the next machine. A rotary and a linear washer need their own handling and interface checks.
Ampoule washing machine testing
For an ampoule washing machine, include the narrow neck, opening, body and base geometry in the sample review. Observe feed-worm, star-wheel and gripper transfers for the selected configuration; do not substitute a similar-volume vial.
Bottle washing machine trial
For a bottle washing machine, confirm the approved material, shape, neck opening, handling parts and drainage requirement. Use the actual bottle format and agreed wash media, then review discharge conditions with the next operation.
What to prepare before the FAT
Write the test scope in a short protocol before the machine trial. Name the container formats, machine model, change parts, wash sequence, utilities, operating conditions, required output and acceptance criteria. Use empty containers in the condition specified for washing, with complete body, neck and opening drawings. Specify any special configuration that affects handling. A generic sample or an unapproved substitute can make a successful trial difficult to interpret.
For process background, the vial washing machine wash-cycle guide explains why RC water, PW, WFI and air stages must be defined as part of the approved process. The FAT should test the agreed sequence for the selected configuration; it should not silently change the process while the machine is being accepted.
10 checks before dispatch
- Freeze the approved scope. Compare the machine offered for FAT with the approved order, URS, layout and drawings. Record the model, container family, format range, handling orientation, process stages, controls and options included in the test. If an option is excluded, mark it clearly instead of allowing the demonstration to imply that it is included.
- Bring approved samples and drawings. Use production-representative vials, ampoules or bottles, in the empty, unfilled condition specified for washing, with complete geometry drawings. Include minimum and maximum formats and any agreed representative/worst-case formats. Record sample identification, supplier or lot reference and the drawing revision used for the trial.
- Verify infeed, transfer and change parts. Check the feed worm, star wheel, mesh conveyor, gripper, pocket, guide, tray or other handling element that belongs to the selected machine. Confirm that the supplied change parts match the approved formats, are identified, and can be fitted and removed as agreed. A single smooth run does not demonstrate every changeover.
- Run the approved wash sequence. Demonstrate each agreed wash and air stage in its documented order. Where the project specifies RC water, PW, WFI or air, record which medium is connected to each stage and what the test protocol asks the team to observe. The FAT confirms operation of the tested sequence; it does not claim that washing alone sterilizes or depyrogenates a container.
- Record utilities and operating conditions. List the water, air, electrical and other services required for the trial, together with the project-defined operating conditions and the instruments used to observe them. Record actual readings when the protocol requires them and identify any condition supplied temporarily for the demonstration. Do not replace a missing utility requirement with an assumed universal value.
- Prove output under agreed conditions. Run the approved sample at the agreed operating pattern and record accepted units, rejected units, stops, jams, operator interventions and the run duration. State the container format, process conditions and options used beside the output. Published model ratings are reference configurations; they are not a guarantee for every size, wash recipe, change part or connected line.
- Test controls, alarms and interlocks. Check start, stop, restart, speed or recipe selection where included, and the alarms or interlocks named in the protocol. Have trained personnel demonstrate the approved scenarios using the machine’s safe test procedure; do not bypass guards or protective functions. Record the machine response, operator message and recovery action. Confirm that an upstream or downstream stop behaves as expected for the defined line interface.
- Inspect the washed containers against agreed criteria. Use the approved visual or process observations for container condition, handling, drainage, wetness, visible residue, orientation and any specified reject response. Record the inspection method and sample basis. Keep microbiological, endotoxin, sterility and depyrogenation requirements under the customer’s approved qualification and laboratory plan unless the FAT protocol expressly assigns a test.
- Review FAT documents and traceability. Check the completed protocol, test sheets, sample references, machine settings, drawings, manuals, certificates, software or recipe records, spare-parts information and change-parts list that the purchase scope requires. Mark each document as supplied, pending or requiring correction. The exact document package should follow the approved order and project scope.
- Close deviations before dispatch release. List every failed observation, substitution, limitation and open action in a deviation or punch-list record. Assign an owner, disposition and retest requirement, then document whether the item is closed, accepted with an agreed action, or blocks release. Dispatch should follow the agreed release process; a signed FAT does not erase unresolved scope or change the later SAT and qualification plan.
Compact preparation and record table
| Prepare before FAT | Record during FAT |
|---|---|
| Approved order, URS, layout, drawings and machine configuration | Model, revision, options tested and any excluded scope |
| Approved samples, format list and representative/worst-case formats | Sample identity, format, change parts and observed handling |
| Wash recipe, utilities and project-defined operating conditions | Connected media, actual readings where required and test conditions |
| Output, quality, alarm and interlock acceptance criteria | Run duration, accepted/rejected counts, stops, alarms and observations |
| FAT protocol, document list and release route | Signatures, deviations, punch-list owner, retest and dispatch disposition |
What the FAT does and does not establish
The FAT is evidence for the configuration, samples and conditions actually tested. It can expose an unsuitable guide, a missing change part, an unclear alarm response or a gap in the document package while the supplier still has access to the machine. It cannot establish performance for an untested container, a later recipe change or a different utility condition.
It also does not prove a sterile manufacturing process. Washing, sterilization and depyrogenation are different operations, with separate acceptance criteria and qualification responsibilities. After installation, the project may require SAT, commissioning, IQ/OQ/PQ or other approved qualification activities. Carry the FAT deviations and agreed actions into that site plan so that the same issue is not lost during handover.
For qualification context, EU GMP Annex 15, sections 3.4–3.7 discusses vendor-site checks against user or functional requirements. Appropriate FAT evidence may support later qualification when justified and unaffected by transport or installation; the site team determines the required follow-up. This article is a practical planning guide, not a project-specific approved protocol.
Frequently Asked Questions
What is a pharmaceutical washing machine FAT?
It is a supplier-site test against an agreed protocol. The team runs approved samples and conditions, observes the machine and records results, documents and deviations before the agreed dispatch decision.
Does a passed FAT prove sterilization or depyrogenation?
No. A washing-machine FAT demonstrates only the tested washing configuration and acceptance scope. Sterilization, depyrogenation, microbiological and endotoxin requirements need their own approved process and qualification plan.
Which samples should the buyer send?
Send production-representative empty containers, current drawings and the agreed washing and handling requirements. Include minimum, maximum and any agreed representative/worst-case formats.
Can the machine ship with an open punch-list item?
Only if the approved contract and FAT protocol allow that disposition. The record should name the deviation, owner, due action, retest or evidence required and whether it blocks dispatch. A signed acceptance should not conceal an unresolved scope question.
Plan a FAT Around Your Actual Containers
Share your vial, ampoule or bottle drawings, samples, required output, wash sequence and acceptance criteria with H M Pharma Machines. The technical team can review the suitable washing-machine configuration and define a practical FAT scope before dispatch.
Request a Technical ReviewExplore Vial Washing Machines